

Every welded H-beam comes out bent
An H-beam welded on a production line is not straight when it leaves the welding station. The four fillet welds along the web-to-flange joints deposit metal on one side of each flange, and as that metal cools it shrinks. The result is a predictable set of distortions: camber along the length, flange rotation (the flanges tilt toward the weld side), and web bowing between the stiffeners.
The amount is not random — it scales with weld volume, flange width and beam length, so it can be allowed for but not eliminated by welding practice alone. That is why a welded H-beam line includes a straightening station, and the HYJ800 is that machine: a straightening machine for H-beam welding lines that brings the finished beam back inside the camber and flange tolerance the specification requires.
What distortion looks like on a welded beam
| Distortion | Cause | Effect downstream |
|---|---|---|
| Camber (longitudinal bow) | Weld shrinkage at the flange-web junction | Beam does not fit between supports; accumulates in a spliced structure |
| Flange rotation / angular distortion | Unequal shrinkage across the flange width | Bolted connections do not seat; the flange face is no longer perpendicular to the web |
| Web bowing | Heat input from both sides plus stiffener welds | Reduces buckling capacity; visible in the finished product |
| Overall length change | Longitudinal shrinkage | Beam is short; splice gap has to be welded rather than fitted |
Of these, camber and flange rotation are the two the straightener addresses directly. Web bowing is normally handled by welding sequence and stiffener placement rather than by straightening — a straightener cannot push a web flat once the flanges are in place.
How straightening works
Two methods are used, and most machines combine or select between them:
- Mechanical (press) straightening — the beam is supported at two points and loaded at a third until the beam yields locally and takes a permanent set that matches the required camber. It is fast, controllable, and requires the operator to know the springback for that section.
- Roller straightening — the beam passes through a set of rolls arranged to bend it alternately in opposing directions, reducing the curvature progressively. Suited to continuous production lines where beams pass through at line speed.
For a welded beam line, roller straightening integrated into the line is the usual choice because it matches the line's throughput; press straightening is used where the section range is wide or the volume does not justify a dedicated roller set.
The measurement problem
Straightening is only as good as the measurement that drives it. On a manual machine the operator measures camber with a wire or a straight edge and adjusts; on a line, in-line measurement after the welding station feeds the straightener setting. Either way, the tolerance has to be defined before the machine is ordered — "straight" is not a specification. Typical structural requirements are expressed as a camber limit over a defined length (for example millimetres per metre), plus a flange rotation limit and a length tolerance.
Where it sits in the line
The sequence on a welded H-beam line is: cut web and flange plate, assemble and tack, weld the four fillet seams (submerged arc, normally with the beam turned), straighten, then convey to drilling, cutting to length or painting. The straightener is the station that makes the downstream operations possible: a beam that is not straight cannot be drilled accurately on a fixed line, and cannot be cut to length square.
Applications
- Construction and bridge fabrication — welded H-beams and plate girders.
- Crane runway beams — where camber affects wheel contact and rail life.
- Machine frames and supports — where flatness of the flange face is functional.
- General structural shops — any welded beam that has to meet a straightness tolerance.
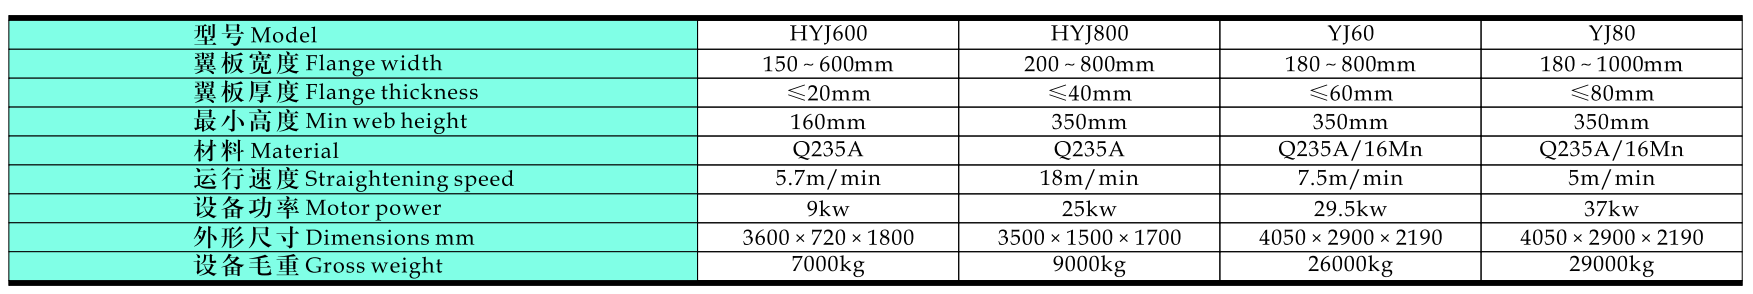
Technical data: HYJ800
| Parameter | Value |
|---|---|
| Web height range | 200 – 1,500 mm |
| Web thickness range | 6 – 32 mm |
| Flange width range | 150 – 800 mm |
| Flange thickness range | 6 – 40 mm |
| Beam length | Up to 15,000 mm |
| Straightening speed | ≈ 18,000 mm/min |
The 18 m/min straightening speed is the number that decides whether the station can keep up with the welding station. A submerged-arc H-beam line welding four fillet seams runs at a travel speed in the same order of magnitude, so a straightener at 18 m/min will not become the bottleneck — but the loading and unloading either side of it can. In a line that has been slowed down unexpectedly, the straightener is rarely the cause; the transfer between stations usually is.
The section range is also worth reading against the welding station's range. A line that welds webs from 200 to 1,500 mm but straightens only to 1,200 mm is a line that produces beams it cannot finish, and that mismatch is much cheaper to find in a specification table than after installation.
Specifying an HYJ800
We need: beam depth and flange width range, web and flange thickness, maximum beam length, material grade, the required straightness tolerance (camber per metre and flange rotation), throughput in metres per shift, whether the machine sits in a continuous line or works as a standalone station, and the available floor length and crane capacity.
Minimum order quantity is 1 set. Standard machines ship in 30–50 days after deposit; line-integrated configurations are scheduled in the technical proposal. Payment terms are T/T; trade terms are FOB, FCA or CIF. Core ranges are CE compliant and supplied against a certificate of compliance.
H-beam line equipment is supplied under the DESAN brand by DESAN ELECTRIC LTD, which has served 1,000+ customers in 20+ countries over 20+ years with welding engineering experience since 1997. For the complete line see the H-beam welding production line; for box sections see the box beam build-up line.